Choosing an Acid Zinc Electroplating supplier is not simply a price comparison. It is a decision about corrosion protection, dimensional control, appearance, and production stability. A bright finish may look impressive under showroom lighting. It may still fail after salt-spray exposure, thread assembly, or storage in humid warehouses.
Industry reports support a careful approach. The U.S. Environmental Protection Agency’s Metal Finishing Effluent Guidelines emphasize controlled chemical management, wastewater treatment, and process monitoring. The European Commission’s Surface Treatment of Metals and Plastics BREF also highlights emission control and documented operating conditions. Meanwhile, the International Zinc Association continues to report zinc’s importance in corrosion protection and material efficiency. These sources do not select a supplier for you. They show why supplier evidence matters.
Frank Altmayer, an AESF Fellow and longtime electroplating educator, has stated, “The best plating process is the one that consistently meets the customer’s requirements.” That principle is easy to repeat. It is harder to verify. Ask for ASTM B633 compliance records, coating-thickness data, hydrogen-embrittlement controls, bath-analysis procedures, and recent salt-spray results. Check whether the supplier tests production parts, not only laboratory panels.
Experience matters here. A capable supplier should explain how barrel plating differs from rack plating, how zinc thickness changes around threads, and how passivation affects color and corrosion resistance. Warning signs include vague certificates, unexplained test limits, and promises of universal performance. Even experienced buyers can overlook packaging and transport conditions. That is worth reconsidering. The right supplier connects chemistry, equipment, inspection, and traceability into one dependable process.
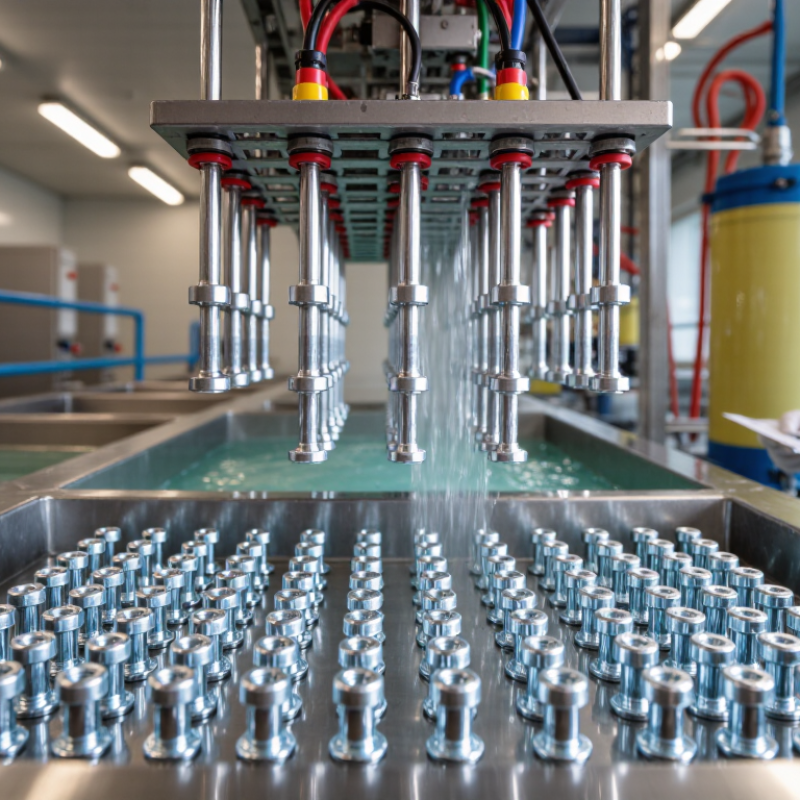
How to Choose an Acid Zinc Electroplating Supplier?
Acid zinc electroplating suppliers provide more than a bright metallic finish. They should offer cleaning, pickling, plating, passivation, drying, and inspection. This complete route reduces peeling, staining, and uneven coverage. The U.S. Geological Survey’s Mineral Commodity Summaries 2025 reports roughly 12 million metric tons of mined zinc in 2024. That scale supports broad material availability, but it does not guarantee process quality. Details matter.
Reliable suppliers provide documented thickness readings, adhesion checks, appearance standards, and corrosion-test results. Ask whether they use calibrated X-ray fluorescence equipment. Request representative salt-spray data under ASTM B117 conditions. The International Zinc Association identifies zinc coatings as an established method for protecting steel from atmospheric corrosion. However, salt-spray hours alone can mislead. Real service conditions include humidity, handling damage, threaded contact, and trapped moisture.
A capable supplier also explains trivalent passivation options, sealers, hydrogen-relief baking, and rack marks before production begins. They should connect each treatment to your substrate, tolerance, and operating environment. Environmental documentation should identify restricted substances and process controls clearly. Ask for batch traceability and corrective-action records. Some suppliers promise identical results across every geometry; that claim deserves questioning. Complex recesses may plate differently. Choose evidence over polished language.
Acid zinc electroplating suppliers should be able to confirm the required coating thickness for each application. The chart shows common ISO 4042 zinc coating designations and their nominal minimum coating thicknesses. When comparing suppliers, also request documentation for passivation, topcoat options, corrosion testing, dimensional control, and environmental compliance.
How to Choose an Acid Zinc Electroplating Supplier?
How to Define Your Plating Requirements
A reliable supplier can only quote accurately when your plating requirements are specific. Start with the base metal, part dimensions, production volume, and surface condition. Steel grades may react differently during cleaning and activation. Share drawings that identify threads, holes, contact points, and areas requiring masking.
Define the zinc coating thickness by function, not appearance alone. For example, state a target range in micrometers and identify critical surfaces. Specify the required corrosion resistance test, inspection method, and acceptance criteria. A bright finish may look attractive, but it cannot replace measurable protection. Choose rack or barrel plating according to part size, shape, and risk of damage. Small fasteners often suit barrel processing, while delicate parts may need rack handling.
Do not overlook post-treatment details. Request the required color, sealant, friction coefficient, and hydrogen embrittlement controls where applicable. Confirm whether threaded parts need dimensional limits after plating. Ask for sample testing, coating-thickness records, bath-control data, and lot traceability. These records show process discipline, not just sales confidence.
Some requirements remain uncertain at the beginning. That is normal. I have seen specifications demand excessive thickness when the real need was better sealing. This raises cost and may affect fit. Review failed samples with the supplier, adjust one variable at a time, and record the result. A practical supplier should explain limitations clearly and recommend a controlled trial before full production.
| Requirement Dimension | Recommended Requirement to Define | Typical Technical Data or Acceptance Criteria | Supplier Evidence to Request | Priority |
|---|---|---|---|---|
| Applicable Standard | Specify the coating standard and revision that will govern production and inspection. | ISO 2081 for electrodeposited zinc coatings on iron or steel, or ASTM B633 for zinc coatings on iron and steel. | Written compliance statement, control plan, inspection procedure, and sample test report. | Critical |
| Base Material | Identify the substrate, material grade, hardness, heat treatment, and any casting or forging condition. | Examples include carbon steel, alloy steel, hardened steel, or high-strength fasteners. Steel hardness and tensile strength may affect hydrogen-embrittlement controls. | Material certificate requirements, pre-treatment compatibility review, and risk assessment for high-strength parts. | Critical |
| Zinc Coating Thickness | Define the minimum local thickness, minimum average thickness, or coating grade required on functional surfaces. | Common project requirements include approximately 5, 8, 12, or 25 µm, but the correct value must be selected according to corrosion exposure and the governing specification. | Coating-thickness records using X-ray fluorescence, magnetic, coulometric, or metallographic methods as applicable. | Critical |
| Corrosion Performance | Define the corrosion test method, duration, specimen condition, and failure criteria. | Neutral salt spray testing may be specified under ASTM B117 or ISO 9227. Set the required hours and white-rust or red-rust limits according to the product environment; there is no universal pass time for every application. | Accredited or controlled laboratory reports, test-panel results, and defined failure photographs or evaluation records. | Critical |
| Passivation or Conversion Coating | Specify the post-treatment required after zinc plating. | Options may include clear, blue, yellow, black, or thick-film trivalent conversion coatings. Define appearance, chemical restrictions, and whether sealing is permitted. | Process description, color or appearance standard, RoHS and REACH declarations where required, and coating-system test data. | High |
| Hydrogen Embrittlement Control | Determine whether the parts require hydrogen relief baking and delayed-load testing. | High-strength steel parts and hardened fasteners require a documented risk assessment. Baking temperature, start time, duration, and test method should be defined by the applicable specification and part condition. | Hydrogen-embrittlement prevention procedure, baking records, lot traceability, and test results where applicable. | Critical |
| Dimensional Control | Identify critical dimensions, threads, holes, fits, masking areas, and allowable dimensional change. | Account for zinc and conversion-coating build-up on threads and precision interfaces. Define masking locations and post-plating gauging requirements. | Process drawings with masking zones, gauge records, first-article inspection, and capability data for critical dimensions. | High |
| Appearance | Define acceptable color, brightness, uniformity, stains, burns, pits, blisters, bare areas, and handling marks. | Use approved visual samples or written limits. Functional surfaces should be free from visible defects that could affect assembly, corrosion resistance, or performance. | Approved limit samples, visual inspection standard, lighting conditions, and defect classification procedure. | Standard |
| Part Geometry and Racking | Provide dimensions, weight, surface area, holes, recesses, sharp edges, and allowable contact points. | Complex geometries can produce non-uniform current distribution and thinner deposits in recesses. Define barrel or rack plating, contact marks, and orientation requirements. | Pre-production review, rack or barrel loading plan, sample parts, and coverage evaluation results. | High |
| Production Capacity | Define annual volume, order quantity, batch size, delivery frequency, and peak demand. | Evaluate whether the supplier can maintain stable process control at the required lot size without excessive lead-time variation. | Capacity statement, typical lead time, production scheduling method, equipment list, and contingency plan. | High |
| Quality Management | Set expectations for process control, nonconforming product, corrective action, and traceability. | Prefer documented quality procedures, calibrated inspection equipment, lot identification, and corrective-action records. Certification requirements should match the risk and industry application. | Quality certificate, calibration records, process-control plan, nonconformance procedure, and sample corrective-action report. | High |
| Chemical and Environmental Compliance | Define restricted substances, wastewater obligations, worker-safety expectations, and documentation requirements. | Confirm compliance with applicable restrictions such as RoHS or REACH. Specify whether hexavalent chromium is prohibited and require confirmation of trivalent conversion chemistry when applicable. | Material declarations, safety data sheets, environmental permits where relevant, and restricted-substance test reports. | Critical |
| Inspection Sampling | Define inspection frequency, sample size, lot definition, and acceptance criteria before quotation. | Use a documented sampling plan based on product risk and customer requirements. Measure coating thickness at agreed locations and test corrosion performance on representative samples. | Inspection and test plan, sampling tables, inspection records, and retained-sample policy. | High |
| Packaging and Handling | Specify protection against scratching, moisture, white corrosion, mixing, and deformation during storage and transport. | Define packaging material, separator requirements, maximum container weight, lot labeling, storage conditions, and shipment identification. | Packaging specification, label sample, logistics procedure, and evidence of controlled storage conditions. | Standard |
| Commercial Evaluation | Compare the total cost rather than only the plating price per part. | Include tooling, masking, testing, sorting, packaging, freight, rework, rejected-part handling, and any minimum order quantity. | Itemized quotation, validity period, tooling ownership terms, payment conditions, and rework or rejection policy. | High |
| Pre-Production Validation | Require sample approval before full-scale production. | Validate coating thickness, appearance, dimensions, corrosion resistance, adhesion where applicable, and assembly performance using production-intent equipment. | First-article report, approved samples, test results, deviation list, and signed production release. | Critical |
Choosing an acid zinc electroplating supplier requires more than a polished certificate. In shop-floor audits, I inspect bath control, test records, and lot traceability. Ask whether technicians monitor zinc concentration, chloride levels, pH, temperature, and brightener dosage. These values affect brightness, thickness, adhesion, and corrosion resistance. The ISO Survey 2023 recorded more than 1.2 million ISO 9001 certificates worldwide. Certification helps, but it does not prove plating competence. Confirm that the certificate covers the actual production site and process.
Technical evidence matters more than confident sales language. Request coating-thickness results using ISO 2178 or ISO 3497 methods. Ask for adhesion testing and neutral salt-spray results under ISO 9227. The AMPP IMPACT study estimated global corrosion costs at 3.4% of worldwide GDP. That figure shows why weak process control becomes an expensive failure. I have seen suppliers pass appearance checks while missing thickness on recessed areas. This is easy to overlook. Review cross-section photos, calibration records, corrective actions, and sample parts from difficult geometries. A supplier should explain hydrogen-embrittlement controls when high-strength steel is involved.
Tips: Visit the plating line if possible. Compare three consecutive production lots, not one sample. Ask technicians to explain a failed test without hiding details. If every answer sounds perfect, investigate further. Real processes have variation. Reliable suppliers measure it, discuss it, and reduce it.
Choosing an acid zinc electroplating supplier requires more than comparing quotation totals. Inspect the complete production line, including tanks, rectifiers, filtration, heating, ventilation, and wastewater controls. Ask for equipment specifications, material details, maintenance records, and recent performance data. A reliable supplier should explain how each system supports coating thickness, appearance, and process stability.
Measure twice. Capacity is never theoretical. Compare the stated hourly output with your actual part size, loading method, rack design, and required coating thickness. A line rated for small fasteners may perform poorly with large, complex components. Request sample trials using representative parts. Check current distribution, bath temperature control, filtration speed, and inspection results. These details reveal more than a brochure.
Cost comparison should include installation, utilities, chemicals, labor, training, spare parts, and downtime risks. A cheaper rectifier may consume more electricity or create uneven deposits. An automated line can reduce labor, but its controls may require specialized support. I have found that production estimates often look optimistic before trial runs. That deserves careful questioning. Ask how the supplier calculates capacity and whether figures include loading, rinsing, inspection, and changeover time. Review references from facilities with similar volumes. Clear documentation, responsive technical service, and honest limitations usually indicate stronger long-term reliability.
Choosing an acid zinc electroplating supplier requires more than comparing coating prices. Ask how the supplier verifies bath chemistry, deposit thickness, adhesion, and hydrogen embrittlement risk. Request recent test reports, calibration records, and traceable lot numbers. A credible supplier explains which standards apply to your part, market, and end use. Do not accept vague claims such as “fully compliant.” Compliance needs evidence.
Review the supplier’s quality system, environmental permits, chemical controls, and worker training records. For regulated applications, confirm current declarations for restricted substances and customer-specific requirements. Arrange a technical call with the plating engineer, not only a sales representative. Ask what happens when thickness drifts, appearance changes, or salt-spray results fail. In a factory audit, I look for labeled tanks, controlled rinsing, and retained production samples. Photos help, but an onsite visit reveals more. If travel is impossible, request a live video walk-through.
Long-term reliability depends on communication after the purchase order. Check response times, corrective-action procedures, spare capacity, and backup plans for chemical or equipment disruptions. Ask whether the supplier can maintain consistent zinc thickness during seasonal humidity and changing production volumes. A useful supplier shares data before problems become urgent. Still, no audit predicts everything. I have seen organized reports hide weak process discipline. That uncomfortable possibility deserves a trial order, defined acceptance limits, and periodic requalification. Keep samples.